
The black mass recovery process capacity of a plant follows the geometry of the shredder, the size of the separation deck and the cooling arrangement of the reactor, and each of those details converts into a tonnes-per-hour figure. You, as an EPC contractor or as a recycling company manager, examine the black mass recovery process capacity against the battery volume of the region before the layout is frozen. A design that balances the three units reaches the declared capacity in normal operation.
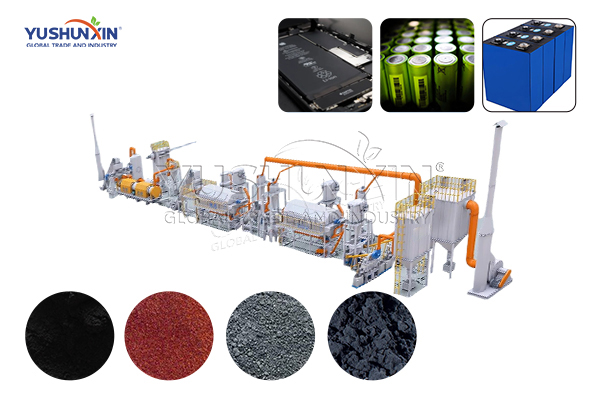
Which engineering details set the shredder throughput?
The rotor diameter, the blade configuration and the discharge screen decide how fast the shredder accepts the packs, and those details depend on the cell format. An engineering details that set black mass recovery capacity review also examines the feeding conveyor, because a narrow belt limits a large rotor. You compare the declared throughput with the throughput at the design density, since a supplier often quotes the lightest material. The throughput of the whole line then follows the slowest unit.
How does the separation stage limit the capacity?
The sieving deck and the density separator process a volume that depends on the particle size, and a coarse product slows the separation. A capacity design for a black mass recovery line sizes the deck for the finest fraction, because that fraction sets the residence time. You measure the screen area per tonne and compare it with the reference plant, and that comparison reveals an undersized deck. The adjustment of the screen then recovers part of the lost capacity.
How does the thermal stage fit the capacity?
A pyrolysis reactor that accepts the shredder output without a buffer forces the whole line to run at the speed of the reactor. A pyrolysis reactor sizing for battery material study defines the residence time and the batch weight, and those two figures set the hourly rate of the thermal unit. You add a buffer silo between the shredder and the reactor, and that silo allows each unit to work at its own rhythm. The capacity then follows the reactor rather than the shredder.
How does the contractor verify the capacity at commissioning?
The performance test runs the line for a full shift with the design feedstock, and the recorded tonnage gives the achieved capacity. You keep the weighbridge tickets and the operating log, because the two records show whether a shortfall comes from the equipment or from the feeding. The contractor then corrects the bottleneck before the handover. The plant receives a measured capacity instead of a catalogue figure.
Conclusion for EPC contractors and recycling companies
Capacity is an engineering result of the rotor, the screen and the reactor, and a balanced design reaches the declared figure during a normal shift. A black mass capacity engineers team that supplies the throughput balance, the layout drawing and the test protocol helps the contractor deliver a plant that meets its guarantee. The supply of spent batteries keeps growing, and a line with a verified capacity serves that supply without idle hours. If your team needs a reference for the process route and the capacity scope, you can learn more about https://www.sxlbp.com/products/500kg-h-lithium-battery-recycling-plant-for-sale/ before the next design review.